-
Cangzhou Datang Pipe Industry Co., Ltd.
-
Tel.:
+86 15100865223 -
Correo:
15100865223@139.com
Tecnología
From base-tube selection to final packing, Datang controls heat-transfer efficiency, fin bonding strength and service life through six key processes. Every process can be adjusted to customer drawings and operating conditions.
01 Base Tube Selection & Incoming Inspection
Carbon steel, 304/316 stainless steel, ND steel, copper or aluminium tubes are selected according to medium, temperature and corrosivity. Every batch is checked for diameter, wall thickness, mill certificate and appearance, so tubes with porosity, cracks or uneven walls never reach the next process.
02 High-Frequency Resistance Welding
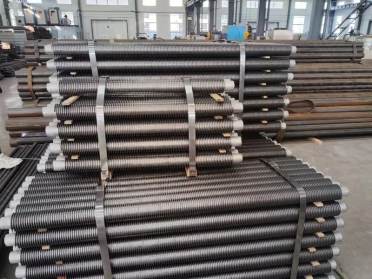
Steel strip and base tube are fed together and fused instantly by high-frequency current, producing a continuous, dense weld. The metallurgical bond gives low contact resistance and stays tight through repeated thermal cycling — the preferred process for high heat-load duties.
03 Laser Welding
The laser beam is concentrated with a small heat-affected zone, producing a narrow, smooth weld — ideal for stainless steel, thin-walled tubes and applications with strict weld appearance requirements. Low distortion and even fin spacing make subsequent galvanizing or pickling easier.
04 Winding & Embedded Fin Forming
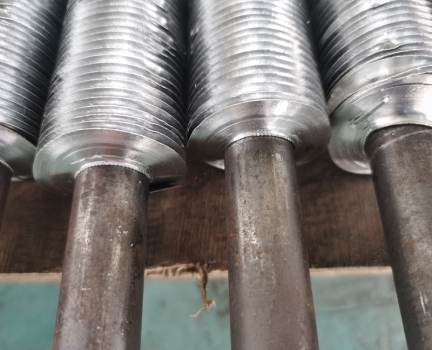
Winding presses aluminium or copper strip continuously onto the base tube; the embedded (G-fin) process seats the fin root into a groove in the tube wall for a mechanical interference fit. Both suit bimetallic finned tubes such as steel-aluminium and copper-aluminium.
05 Heat Exchanger Assembly
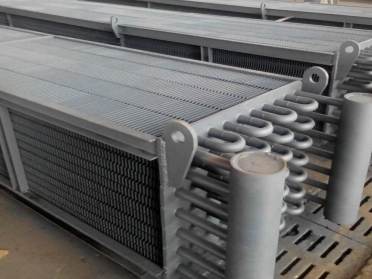
Tube arrangement, fin pitch and face area are determined by thermal calculation, followed by bending, welding, tube-sheet assembly and flange connection. Heat exchangers, radiators, air coolers, economizers and condensers are all built to duty and hydro-tested before delivery.
06 Final Inspection & Packing
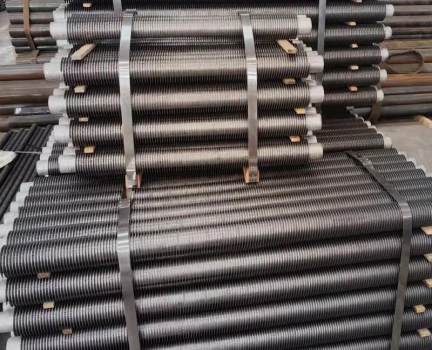
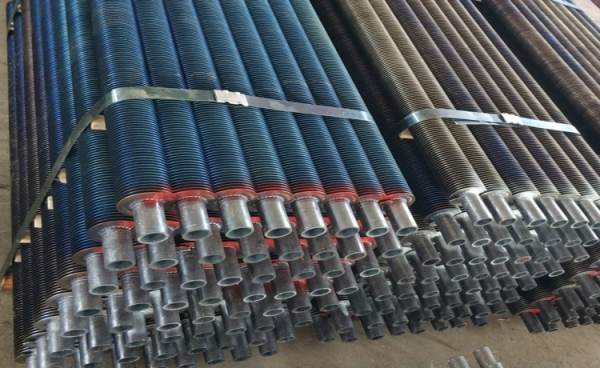
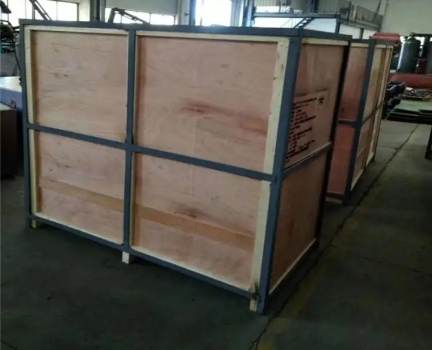
Each piece is inspected for fin spacing, weld appearance, tube-end dimensions and surface treatment; critical parts undergo air-tightness or hydrostatic testing. Approved units are galvanized or anti-rust coated, wrapped in protective film and packed in wooden cases or steel straps for long sea freight.


